Crimping vs. Ultrasonic Welding for EV Charging Cable Terminations
Oct 12, 2026
The connection between a charging cable and its power contact is part of the current path. If the joint adds resistance, it can generate localized heat. If it lacks mechanical strength, it may also become unstable during service.
Crimping and ultrasonic metal welding are both used for cable-to-contact connections. The right method depends on the contact design, conductor construction, available space, and how the process can be controlled and verified.
This article covers the connection between the cable conductor and the rear of the contact. It does not cover the mating interface between the charging connector and vehicle inlet.
Crimping: Compression Around the Conductor
In a crimped termination, a tool compresses the contact’s crimp barrel around the conductor. The joint must provide electrical continuity while holding the conductor securely.
The contact and conductor need to be matched, and the crimp process needs to be controlled. Relevant factors include conductor cross-section and strand construction, barrel dimensions, die selection, crimp height, wire position, and strand condition.
An under-compressed or poorly matched crimp may not retain the conductor securely. Excessive compression can damage strands or deform the contact. A crimp’s appearance alone does not show whether it meets its electrical and mechanical requirements.
Ultrasonic Welding: A Solid-State Joint
Ultrasonic metal welding joins the conductor to a compatible contact surface using pressure and high-frequency mechanical vibration. The process does not use solder or filler material. It requires a suitable welding area and a fixture that holds the parts in position.
Conductor material and strand arrangement, contact geometry, weld area, fixture design, and process settings all affect the result. The welding process needs a defined operating window, with checks suited to the joint design.
What the Two Methods Require
Consideration
Crimping
Ultrasonic welding
Joint formation
Contact barrel is compressed around the conductor
Pressure and vibration form a solid-state metal joint
Contact geometry
A barrel designed to deform around the conductor
A suitable welding surface and access for the tool and fixture
Process controls
Die, crimp height, force, conductor position, strand condition
Energy, pressure, vibration, time, positioning, fixture condition
Possible checks
Dimensions, visual inspection, cross-section, pull force
Process records, visual inspection, cross-section, pull force
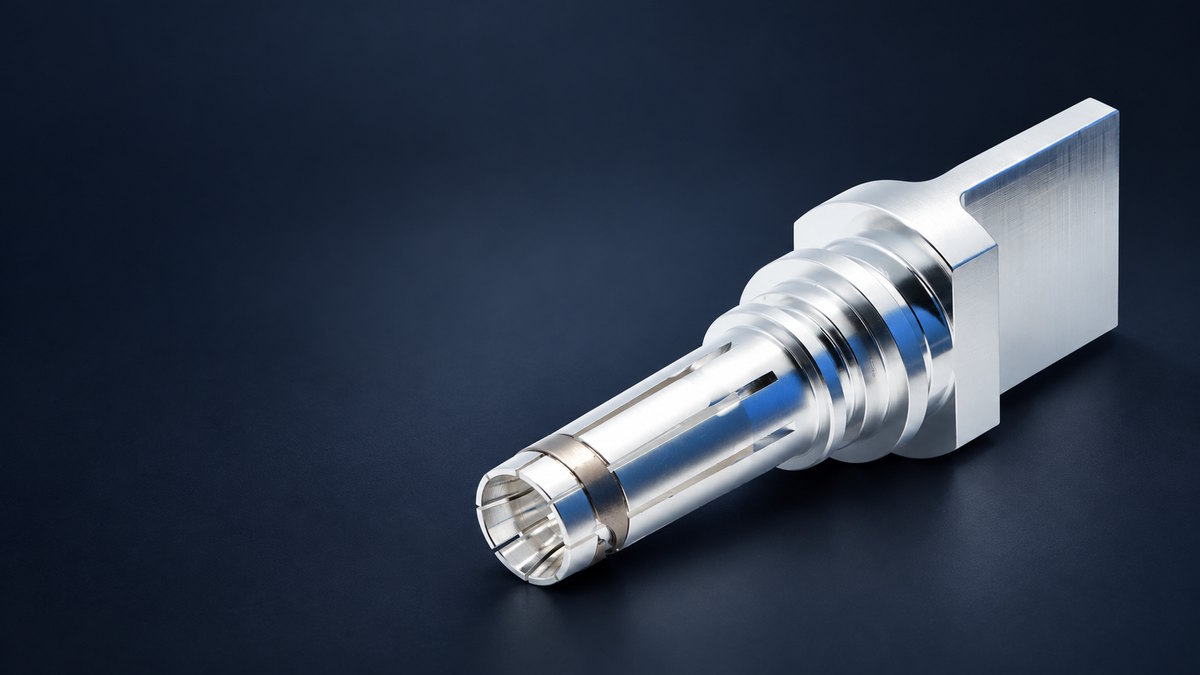
Consider two contact designs. One has a closed crimp barrel sized for a defined conductor; its process controls may include wire-and-die matching and crimp-height checks. Another has a flat termination area designed for ultrasonic welding, where the weld area, conductor position, and welding parameters become key controls.
These designs show why the joint geometry guides the process choice. Either method may produce an acceptable connection when the contact, conductor, and process are matched. The finished assembly still needs to meet its electrical and mechanical requirements.
Resistance and Heat at the Termination
Resistance at the conductor-to-contact joint contributes to heat when current flows through it. Inconsistent contact within the joint, damaged strands, or unsuitable geometry can affect resistance.
For example, a joint resistance of 0.1 mΩ at 300 A would dissipate 9 W, based on P=I2RP=I^2R. This is an illustrative calculation, not a product test result. It describes electrical power dissipated at the assumed resistance; it does not predict temperature rise. The actual temperature depends on the complete assembly and how heat moves through it.
A low initial resistance reading also does not establish long-term performance. The assembled connector should be tested under conditions relevant to its intended use, with consistent measurement methods and defined test points.
Choosing a Method for the Contact Design
Start with the contact’s rear geometry and the cable conductor. The chosen process has to suit the conductor’s size and strand construction, fit the available assembly space, and work with the way the connector is assembled.
Production volume and process control matter as well. Crimping and ultrasonic welding use different tooling and process checks. The method needs to be repeatable for the intended production process.
Rated current is one part of the application, but it does not determine the termination method on its own. The contact, conductor, assembly, and thermal requirements have to be considered together.
Verifying the Finished Joint
Possible checks include visual and dimensional inspection, crimp-height or weld-area assessment, cross-section inspection, pull-force testing, resistance measurement, and temperature-rise testing. The appropriate combination depends on the joint design and validation plan.
These tests answer different questions. A joint may meet its pull-force requirement while still needing separate resistance and temperature-rise tests. Mechanical retention alone does not establish electrical performance.
For production validation, testing may also be repeated after relevant aging or environmental exposure. Acceptance limits and test conditions should be defined for the specific contact and cable assembly; results from one design do not automatically apply to another.
Matching the Termination to the Contact
Crimping and ultrasonic welding can both be suitable for EV charging cable terminations. The contact geometry and conductor construction define which process can be used; testing shows whether the finished joint meets its requirements.
Workersbee supports custom EV charging contacts based on a drawing, sample, or existing connector. Contact geometry and conductor-connection requirements can be reviewed as part of the project. See EV charging connector contacts.
Read More



 English